





Deep Dive into Sintered Wire Mesh Candle Filters: The Ultimate Guide
In the world of industrial filtration, achieving a perfect balance between high efficiency, robust durability, and consistent performance is the ultimate goal. Among the myriad of filtration solutions available, one technology stands out for its unique construction and superior capabilities: the sintered wire mesh Candle Filter. This article provides a comprehensive exploration of this advanced filter, delving into its manufacturing process, key characteristics, and the diverse industrial applications it serves.
Understanding the Fundamentals: What is a Sintered Candle Filter?
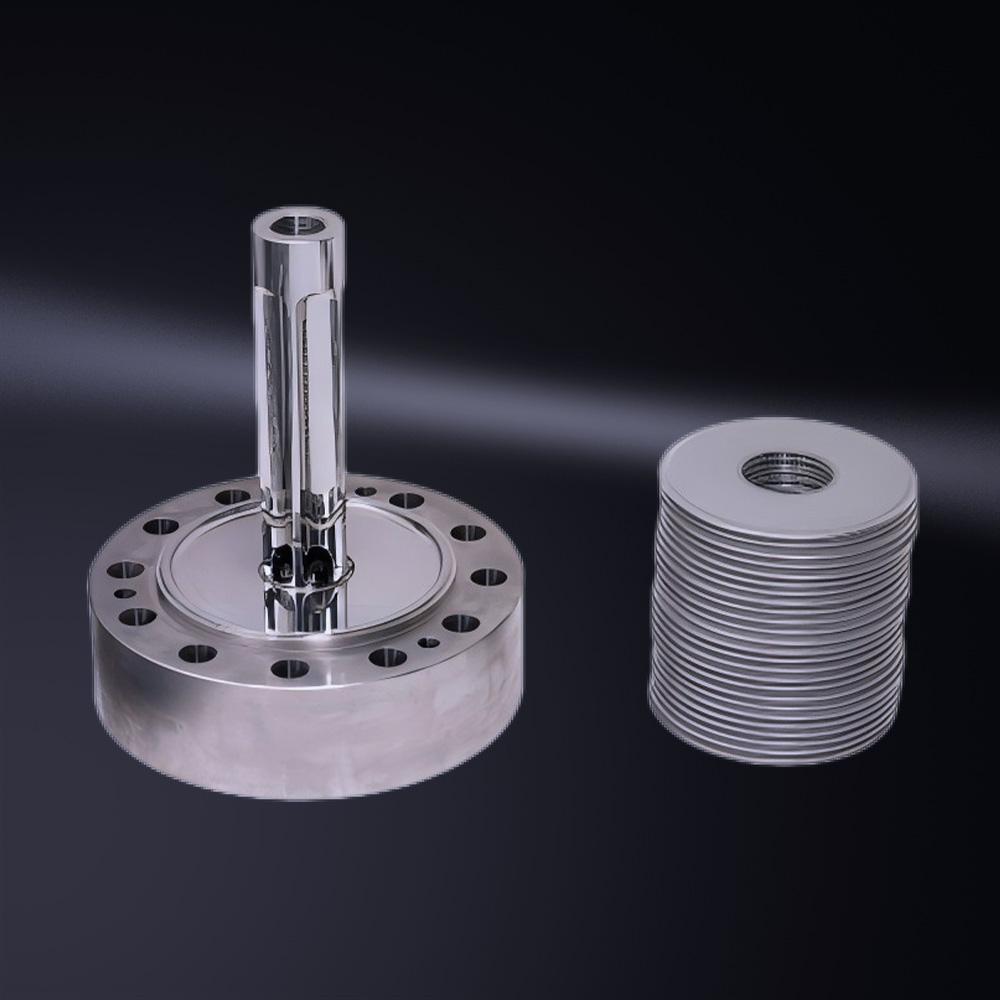
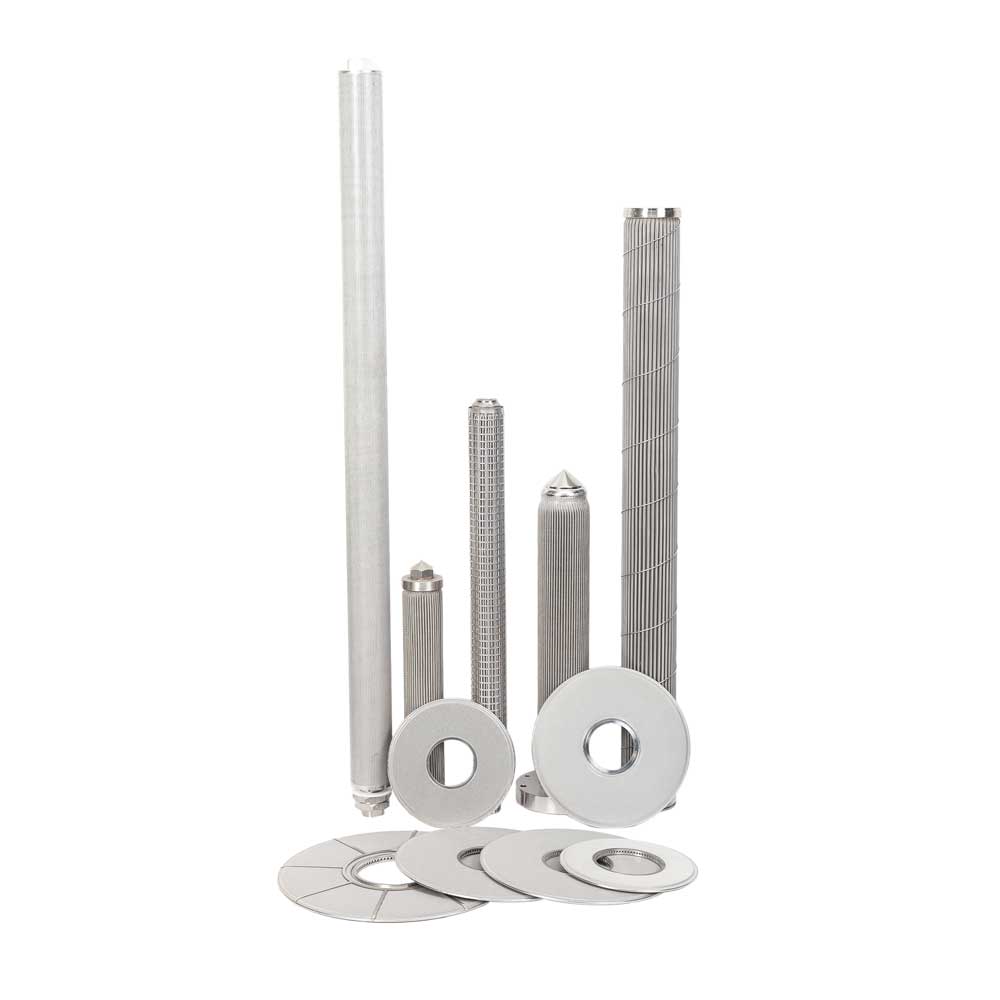
A sintered wire mesh candle filteris a type of rigid, self-supporting Filter Element characterized by its cylindrical, candle-like shape. Unlike conventional woven wire mesh, its core strength lies in the sophisticated sintering process it undergoes. Sintering involves stacking multiple layers of precise woven wire mesh and heating them in a controlled, high-temperature furnace to a point just below the metal's melting point.
This critical thermal treatment causes the contact points between the wire meshes to fuse and bond metallurgically, creating a single, monolithic porous structure. The result is not a simple layered mesh, but a unified filtration media with exceptional strength and precisely engineered pore structures. This fundamental manufacturing difference is what sets sintered candle filters apart, granting them a unique set of advantages for demanding industrial environments.
Key Characteristics and Technical Advantages
The sintered manufacturing process imparts a range of beneficial properties that make these filters a preferred choice for critical applications.
-
High Mechanical Strength and Structural Stability: The diffusion-bonded structure creates an incredibly robust filter that can withstand high differential pressures without collapsing or deforming. This makes it ideal for applications involving significant pressure surges or cyclic loading, where pleated or cartridge filters might fail.
-
Precise and Consistent Filtration Performance: By utilizing woven mesh as a base material, manufacturers can control the pore size with high accuracy. The sintering process locks this precision in place, ensuring a uniform pore distribution across the entire filter surface. This consistency guarantees reliable particle capture and prevents the unpredictable bypass common in less uniform media.
-
Excellent Flow Rates with Low Pressure Drop: The rigid, porous structure provides a high proportion of open volume, creating minimal resistance to fluid flow. This allows for high flow rates while maintaining a low initial pressure drop, leading to improved system efficiency and reduced energy consumption over the filter's lifespan.
-
Robust Cleanability and Reusability: Sintered wire mesh filters are designed for longevity. Their sturdy construction allows them to withstand repeated and aggressive cleaning methods, such as high-pressure backwashing, ultrasonic cleaning, or chemical rinsing. This effective cleanability enables multiple reuse cycles, significantly reducing operating costs and waste generation compared to disposable filters.
-
Broad Material and Temperature Compatibility: These filters can be manufactured from a variety of metal alloys, including stainless steel (304, 316L), Hastelloy, and Inconel. This allows for compatibility with a wide spectrum of process fluids—from water and oils to aggressive acids and alkalis—and operation in extreme temperature conditions, from cryogenic to high-heat environments.
Industrial Applications: Where Sintered Candle Filters Excel
The unique combination of strength, precision, and durability makes sintered candle filters indispensable across numerous high-stakes industries.
-
Chemical and Petrochemical Processing: They are crucial for catalyst recovery, polymer filtration, and the purification of aggressive chemicals, where resistance to corrosion and high pressure is paramount.
-
Oil & Gas: Used in upstream and midstream processes for protecting equipment, dehydrating crude oil, and filtering various process gases and liquids under extreme conditions.
-
Pharmaceutical and Food & Beverage: In sterile processes, their cleanability and ability to be validated for consistent pore size make them suitable for clarifying APIs, sterilizing gases, and filtering critical process fluids.
-
Power Generation: They protect turbines and critical systems by removing particulate matter from fuel and lube oils, ensuring uninterrupted and efficient operation.
-
Water and Wastewater Treatment: Employed in advanced treatment systems for final effluent polishing and the removal of fine suspended solids.
Conclusion
Sintered wire mesh candle filters represent a pinnacle of engineering in solid-liquid and gas-solid separation. Their monolithic structure, born from the precise sintering process, delivers an unmatched blend of precision, strength, and long-term economic value. For industries where filtration performance, system reliability, and total cost of ownership are critical, understanding the deep-seated advantages of this technology is the first step toward optimizing operations.
If your processes demand a filtration solution that can endure challenging conditions while providing consistent, high-quality results, exploring the specifications of sintered wire mesh candle filters is a compelling next step.
