





How to select the pore size and structure of the filter element based on your polymer type and pollutant characteristics?
The technical director of an injection molding factory in Detroit recently discovered that the black spot defect rate on the ABS production line had soared to 3%, while the PET production line was operating smoothly. The problem ultimately points to the same root cause: they used the same specification of filter elements for the two polymers. This detail reveals a common misconception - in the field of Polymer Filtration, a universal solution often implies systemic risks.
The flow characteristics of polymers are the underlying logic
The difference in melt index directly determines the basic structure of the filter element. The viscosity of highly fluid nylon 66 is less than 500 Pa·s at 280℃, and the melt can easily pass through the dense sintered metal felt structure. The viscosity of PC/ABS alloy may exceed 2000 Pa·s at the same temperature. Forcing the use of high-precision filter elements will only lead to a sudden increase in pressure and shear degradation. The experience of a certain modified plastic factory in the Netherlands is that when dealing with high-viscosity materials, increasing the effective filtration area of the filter element by 40% is more reliable than simply enlarging the pore size. This way, it can be maintained
Youdaoplaceholder0 retention efficiency without causing the melt to remain on the surface of the filter element for too long.
Heat-sensitive materials bring another consideration. PVC is extremely sensitive to shear heat within the processing window. The multi-layer progressive filter element structure is more suitable than the single-layer absolute precision filter element. The outer 20-micron coarse Filter Mesh first intercepts large impurities, while the inner 5-micron fine medium deals with tiny particles. This layering strategy prevents local overheating caused by all dirt being clogged at a single level. Data from a German extrusion equipment manufacturer shows that the progressive structure can extend the filter element replacement cycle of the PVC production line by 2.3 times.
The characteristics of pollutants determine the aperture accuracy
Gel is the most troublesome pollutant in the processing of polyolefins. This type of soft aggregate will deform and squeeze through the filter core under pressure fluctuations. On the surface, the filtration efficiency seems to meet the standards, but in fact, fisheye defects will still appear on the product surface. For gels, a nominal accuracy of 0.5 microns is more effective than an absolute accuracy of 5 microns - the key lies in the depth interception capacity of the filter medium rather than the surface pore size. After a Singaporean film manufacturer switched to deep-wound filter cartridges with a fiber diameter of 2 microns, the gel penetration rate dropped from 15% to less than 1%.
The physical form of metal shavings is completely different. These hard particles mainly come from the wear of the screw and the cylinder, and their particle size distribution is usually in the range of 5 to 50 microns. Rigid particles require absolutely precise filter elements because once they penetrate, they cannot be remedied. The approach taken by Japanese engineering plastic suppliers is to install magnetic separators upstream of the filter elements as pre-filters, reducing the concentration of metal particles from the ppm level to the ppb level. As a result, the lifespan of the 10-micron absolute precision filter elements downstream can be extended by 5 to 8 times.
The treatment of moisture and gases is often overlooked. PET and PU are extremely sensitive to residual moisture, but this is not a problem that can be solved by the pore size of the filter element. The lesson from a Monterey auto parts supplier was that they overinvested in the desiccant filter element but neglected the maintenance of the vacuum degassing device, and as a result, the acetaldehyde content in the preform still exceeded the standard. The correct logic is that the filter element is responsible for solid-liquid separation, and the gas and water need dedicated processing units to work in coordination.

Multi-dimensional balance of filter element structure
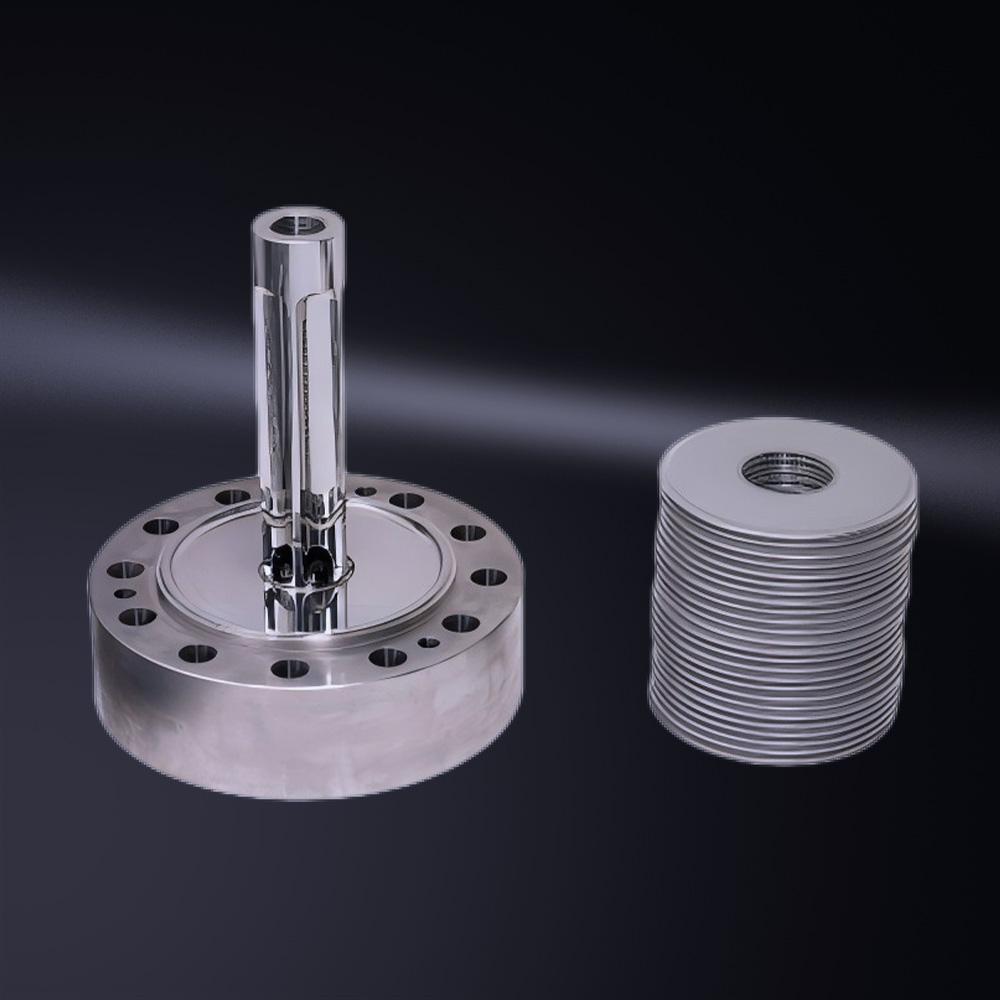
The choice between candle filter elements and disc filter elements is essentially a trade-off between economy and precision. Candle filter elements provide a larger filtration area within a unit volume and are suitable for continuous production. Disc filter elements can achieve higher precision and cause less material loss when replaced. A large film factory in the Midwestern United States adopted a hybrid strategy: candle filters were used for the main filtration to ensure production capacity, and disc filters for the final filtration to guarantee quality. These two checkpoints increased the overall yield by two percentage points.
Material compatibility is more complex than people imagine. During the processing of fluoropolymers, conventional stainless steel filter elements may be corroded, and the iron ions precipitated in turn catalyze the degradation of the polymers. After a special materials company in Turin switched to Hastelloy alloy filter elements, it not only solved the corrosion problem but also found that the yellowing index of its products improved by 30%. This kind of implicit benefit can often only be quantified through destructive testing.
The layout of differential pressure monitoring points directly affects the quality of decision-making. Most factories only install pressure gauges at the inlet and outlet of the filter, which can only reflect the overall clogging situation. Research from the Technical University of Munich shows that adding pressure sensors at 1/3 and 2/3 of the filter element length can predict filter element failure 4 to 6 hours in advance, avoiding sudden shutdowns. This predictive maintenance approach is rewriting the logic of spare parts inventory.
The non-negligible nature of environmental variables
Fluctuations in environmental temperature can alter the actual viscosity of polymers. In Saudi Arabia, the temperature difference of 45℃ during the day and 25℃ at night causes the melt pressure of the PP production line to fluctuate by more than 15 bar, and the effective particle size retention of the filter element drifts accordingly. The solution is to install an insulating jacket on the filter housing to keep the temperature fluctuation within ±3℃, so that the selection parameters of the filter element can be stable and reliable.
Altitude affects the vacuum degassing effect and indirectly influences the load on the filter element. Mexico City is located at an altitude of 2,240 meters. A local pipe factory found that with the same PE raw material, the filter element lifespan was 30% shorter than that of factories at sea level. The fundamental reason is that under low pressure, degassing is incomplete, and more gas is carried by the melt to the surface of the filter element to form bubbles, accelerating the formation of the filter cake layer. This reminds purchasers that when providing process parameters to filter element suppliers, local air pressure data must be included.

The decision-making framework in practical operation
Don't rush to ask about the filter element specifications. Conduct a comprehensive pollutant audit first. Collect impurity samples within 24 hours and determine the composition and particle size distribution by microscopic and spectral analysis. A Dutch recycled material processing company's approach is that for each batch of rPET raw materials it receives, it quickly hot-presses 10 sample pieces and counts the number of black spots. This data directly guides the filter element configuration - when the number of black spots is greater than 100 per square meter, a 3-micron filter element is used; when it is between 50 and 100 per square meter, a 5-micron filter element is used; and when it is less than 50 per square meter, a 10-micron filter element is used.
It is more important to establish a dynamic adjustment mechanism. A certain packaging film factory in the Netherlands stipulates that after each change of polymer grade, the products within the first four hours should be stacked separately. After inspection, it will be decided whether to mix them into the normal batch. This caution may seem to increase the workload, but in fact, it avoids the scrapping of entire batches worth tens of thousands of euros.
The selection of the pore size and structure of filter elements is never an isolated technical decision, but a systematic consideration embedded throughout the entire process chain. The next time you face a supplier's technical manual, you might as well lay out your material safety data sheet, workshop temperature and humidity records, and even shift schedules on the desk. The real solutions are often hidden in those seemingly unrelated details.