





0102030405
Middle East Spunbond Nonwoven Plant Candle Filter Selection Guide: In-Depth Analysis for Different Spinning Process Requirements
2026-03-31
Middle East Spunbond Nonwoven Plant Candle Filter Selection Guide: In-Depth Analysis for Different Spinning Process Requirements
In the rapidly developing spunbond nonwoven industry in the Middle East, melt filtration is the lifeline for ensuring stable production line operation and final product quality. As a core component in this process, the selection of Candle Filters is by no means a "one-size-fits-all" approach. Different spinning processes (such as spunbond, meltblown, SMS composite, etc.) have drastically different requirements for polymer melt purity, fluidity, and pressure stability. This guide aims to provide a clear framework for plant decision-makers, process engineers, and procurement managers in the Middle East, offering in-depth insights into how to select and adapt the most suitable candle filters based on the specific needs of different spinning processes, thereby achieving dual optimization of production efficiency and product quality.
Understanding Melt Filtration Challenges in Spunbond Nonwoven Production
The core of the spunbond process involves melting polymers (such as PP, PET), filtering, metering, extruding through spinnerets, drawing, web laying, and bonding to form nonwovens. During this process, any tiny gels, carbonized particles, or impurities can cause spinneret clogging, filament breakage, and even fabric defects, seriously affecting production continuity and product qualification rates. Therefore, an efficient and reliable melt filtration system is indispensable.
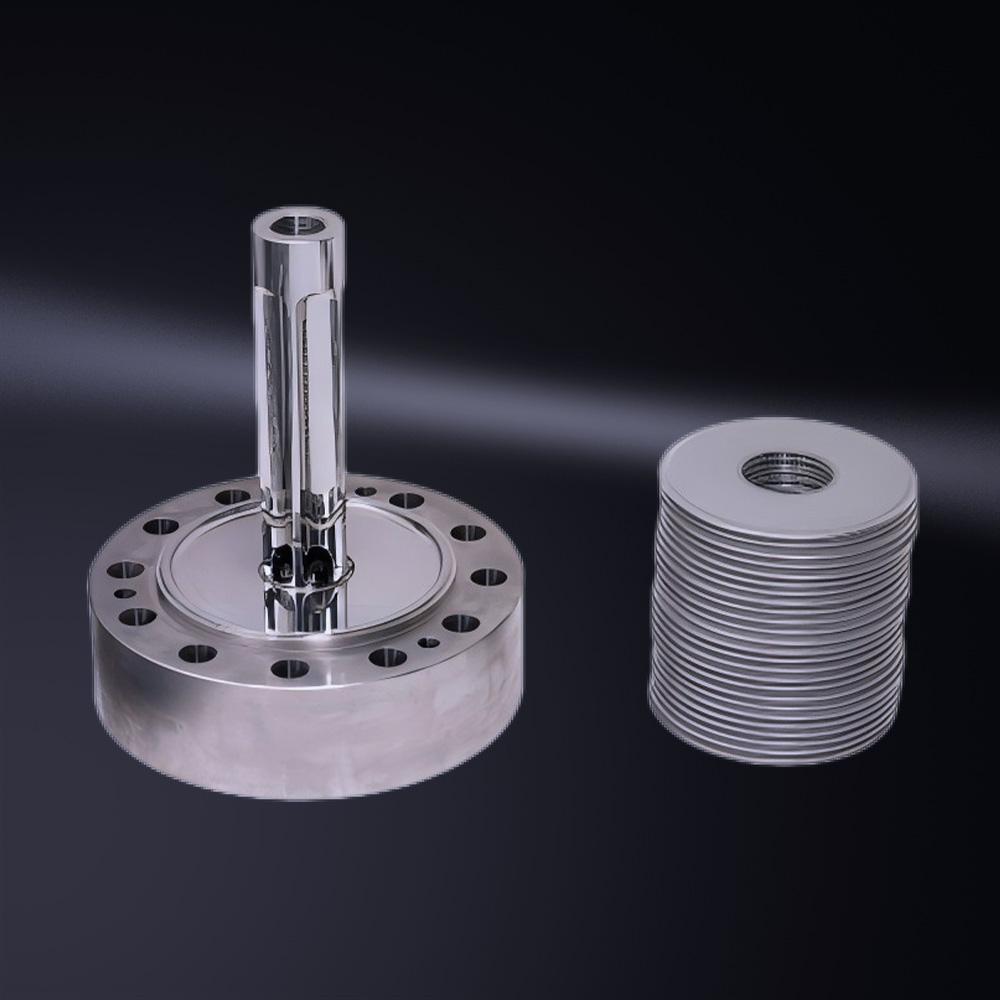
The role of candle filtersis to provide the final, most precise "check" for polymer melts before they enter the spinning assembly. However, the challenge lies in that different processes have varying requirements for filtration precision, dirt-holding capacity, pressure rise rate, and chemical corrosion resistance. An incorrect selection can lead to frequent Filter Element replacement, production interruptions, increased energy consumption, or failure to meet the technical specifications of the target product.

Detailed Guide to Core Spinning Processes and Candle Filter Adaptation Techniques
The following details the process characteristics and specific requirements for candle filters for several mainstream spinning processes in the Middle East.
1. Conventional Spunbond Process
Process Characteristics: This is the most basic and widely used process. It features fast production speed, high requirements for fiber uniformity and strength, relatively stable melt temperature, and large processing capacity.
Core Requirements for Filters:
- High Dirt-Holding Capacity: Due to large output, the filter must carry a large amount of impurities to extend the replacement cycle and reduce downtime.
- Stable Initial Pressure Difference: The initial pressure difference of the filter must be sufficiently low to ensure stable and uniform distribution of melt to each spinning position, which is the foundation for ensuring web uniformity.
- Medium to High Filtration Precision: It usually needs to effectively intercept particles above 20-40 microns to prevent clogging of spinneret capillaries.
Adaptation Techniques: Prioritize candle filter elements with a multi-layer composite structure. For example, filter elements composed of a support mesh, high-precision filtration layer, and pre-filtration layer. This structure can capture large impurities through the pre-filtration layer to protect the precision layer, and achieve final filtration through the high-precision layer, significantly improving dirt-holding capacity and service life while maintaining high precision. Pleated candle filters are an excellent choice for this process due to their large effective filtration area.
2. Fine Denier/Ultra-Fine Denier Spunbond Process
Process Characteristics: Produces finer fibers to obtain softer nonwovens with higher specific surface area (such as high-end wipes and medical dressings). The spinneret holes are extremely small, requiring extremely strict melt purity.
Core Requirements for Filters:
- Ultra-High Filtration Precision: This is the primary requirement, usually needing to stably intercept particles of 10-25 microns or smaller. Any missed impurities can easily cause spinneret hole clogging.
- Excellent Fiber Separation and Deep Filtration Capacity: The filter material needs to not only perform surface interception but also capture finer gels through its internal three-dimensional structure.
- Stable High-Pressure Bearing Capacity: To achieve high precision, the filter element itself will bring higher resistance, so it must ensure structural integrity under high pressure without fiber migration.
Adaptation Techniques: Must use candle filter elements made of stainless steel sintered fiber felt or multi-layer special metal woven mesh. These materials can provide a stable and uniform microporous structure, which is the guarantee for achieving ultra-high precision and deep filtration. Avoid using single woven mesh filter elements, as they may have dimensional instability or "window effect" under high pressure. The end cap sealing and support structure of the filter element must be of heavy-duty design.

3. SMS (Spunbond-Meltblown-Spunbond) Composite Process
Process Characteristics: Combines spunbond layers with meltblown layers, featuring both strength and filtration/barrier performance. The production line includes a meltblown die, which is much more sensitive to impurities than spunbond dies. The polymer molecular weight used in the meltblown process may vary, and the process temperature window is narrow.
Core Requirements for Filters:
- Extreme Protection for Meltblown Layers: The filter selected for the meltblown line should refer to the "fine denier spunbond" or even higher standards in terms of precision and reliability, because the meltblown fiber diameter is only 1-5 microns, and any impurities will cause die streaks or web breaks.
- Thermal Shock and Thermal Stability: Temperature fluctuations may occur during material change or process adjustment in SMS production lines, and the filter element material must withstand repeated thermal cycles without failure.
- Independent Line Filtration Strategy: It is advisable to configure independent or different specifications of filtration systems for the meltblown line and spunbond line, so as to accurately select and manage according to the severity of each process.
Adaptation Techniques: Configure ultra-high precision sintered metal fiber felt candle filter elements for the meltblown line. For the spunbond layer, select conventional high dirt-holding capacity filter elements according to the final product requirements. Consider using a protective mesh with a higher mesh count to prevent fiber migration of the filter material itself under extreme working conditions. When communicating with suppliers, it is necessary to clearly state that it is used for the SMS composite process, especially the meltblown section.
4. Bicomponent Spunbond Process
Process Characteristics: Uses two different polymers (such as PP/PE, PET/CoPET) for side-by-side or sheath-core structure spinning. The process is complex, and the two component melts may have different rheology, viscosity, and thermal history, making it easy to generate new types of gels at the mixing interface.
Core Requirements for Filters:
- Targeted Filtration for Specific Gels: The filter element needs to effectively filter new, possibly more viscous gel particles generated due to incompatibility or uneven mixing of the two polymers.
- Material Compatibility: The filter element material (such as stainless steel grade) must have good compatibility and corrosion resistance with both polymers and their possible additives (such as hydrophilic masterbatches, color masterbatches).
- Consistent Filtration Performance: Ensure that the two component melts have similar purity after filtration to avoid structural defects of composite fibers.
Adaptation Techniques: Conduct in-depth process consultation with filter suppliers. Provide the specific grades, mixing ratio, and processing temperature of the two polymers. Suppliers may recommend special filter materials with specific pore size gradients or surface treatments to optimize the capture efficiency of impurities in the mixed system. Regular post-filtration melt analysis to monitor gel types and quantities is the key to optimizing the filtration scheme.

Choosing the Best Partner for Your Plant: Beyond the Product Itself
Selecting a candle filter is not just buying a "component", but choosing a long-term partner that can provide process solutions. An excellent supplier should be able to:
- Provide Customized Design: According to your specific spinning process, polymer type, and production capacity, recommend the most suitable filter material combination (woven mesh/sintered mesh/fiber felt), precision gradient, size, and interface form.
- Share Industry Knowledge and Data: Provide filtration performance data and cases of similar process applications to help you predict filter element life and pressure rise curves.
- Support Localized Services: Have fast-response technical support and spare parts inventory in the Middle East to minimize production loss caused by filtration problems.
- Conduct Failure Analysis: Analyze used filter elements, diagnose impurity sources, and reverse optimize your front-end raw materials or process parameters from the perspective of filtration.
Conclusion
In the increasingly competitive spunbond nonwoven market in the Middle East, adapting candle filters to specific spinning processes through refined selection is an important lever to reduce costs, improve efficiency, and enhance product competitiveness. From the high dirt-holding demand of conventional spunbond, to the extreme precision requirements of fine denier and meltblown processes, and the compatibility challenges of bicomponent spinning, each process calls for a tailor-made filtration solution.
It is recommended that when communicating with suppliers, you clearly elaborate on your process type, product positioning, and specific challenges, rather than just asking for "filter prices". Through this cooperation based on in-depth process understanding, the candle filter you choose will be transformed from a cost expenditure into a reliable asset that ensures the excellent operation of your production line.