





0102030405
Screen Filter Selection Guide: Matching Tips for Plastic & Rubber Recycling & Pelletizing Plants
2026-05-25
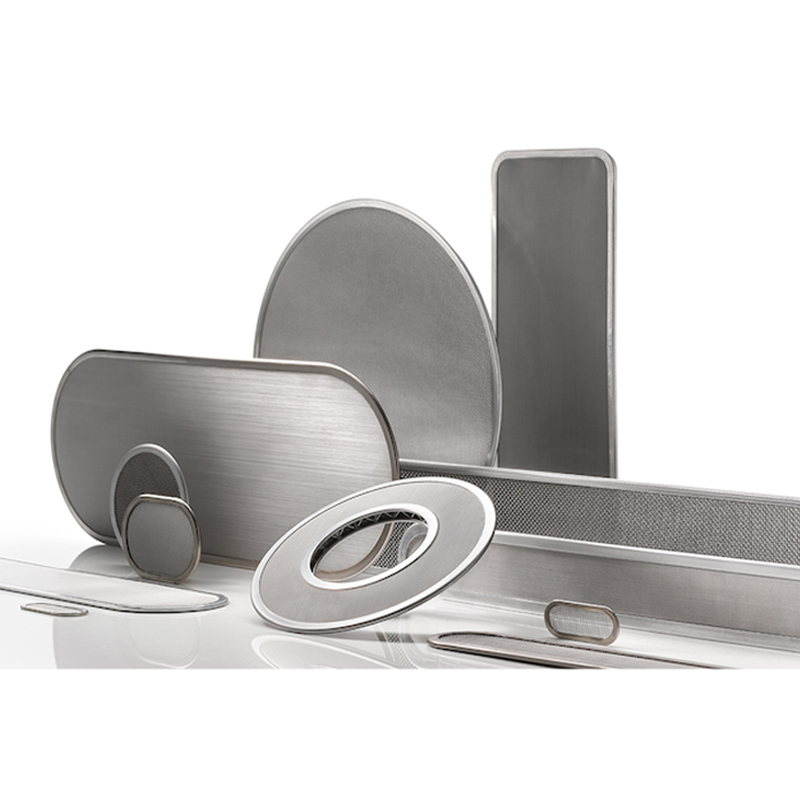
In plastic or rubber recycling and pelletizing processes, impurities in the melt — such as unmelted materials, gel particles, metal chips, and carbides — directly affect the purity, color, and mechanical properties of final pellets. As the most basic and flexible filtration component, Screen Filters (usually stainless steel wire mesh filters) act as a critical gatekeeper in production. However, recycled materials vary greatly in characteristics; choosing the wrong mesh count, structure, or installation method can lead to frequent screen changes, sharp output drops, or excessive filter consumption.
This guide is specially written for procurement and production supervisors of recycling and pelletizing plants. It provides a logical selection framework for screen filters based on actual material properties.
I. Material Analysis: Diagnose Your Feedstock Impurity Profile First
Different recycled materials differ completely in impurity form and melt index — this is the primary principle of selection. Match your core raw materials below:
| Recycled Material Type | Typical Impurity Characteristics | Core Challenges for Filters |
|---|---|---|
| PE Film (Agricultural / Packaging Film) | Fine sand, plant fibers, oligomer gels | High content of fine impurities, easily causing rapid clogging of the surface filter layer |
| PP Woven Bags | Printing ink, label paper fibers, aluminum foil fragments | Fiber impurities easily penetrate or wrap around filter edges |
| PET Flakes | Label pulp, aluminum chips, PVC impurities | High melting point, high impurity density, demanding high filter strength |
| Rubber (EPDM / NBR) | Vulcanized rubber particles, metal chips, carbon black agglomerates | Extremely high viscosity, requiring large filtration area and rigid support |
Key Judgment: If your impurity content exceeds 0.5% by weight, or particle size varies widely (from 50 microns to 2 mm), a single plain woven screen filter may not be optimal. Consider combined configurations or upgrading to pleated filters.
II. Filter Precision: Balance Between Purity & Output
The precision of screen filters is usually expressed in mesh count (number of openings per linear inch). For recycling and pelletizing, there is no “best mesh” — only the most suitable range.
- Coarse Filtration (20–60 mesh) Suitable for large-scale rubber pelletizing or heavily contaminated rigid plastic scrap. Mainly intercepts visible large impurities to protect downstream equipment (gear pumps, die heads). Pressure rises slowly, with relatively long screen replacement cycles.
- Medium Filtration (80–120 mesh) The mainstream choice for general recycling pelletizing. Captures most gels and fine sand, producing pellets ideal for injection molding, film blowing, and other applications sensitive to black spots.
- Fine Filtration (150–200 mesh) Used for high-end film or chemical fiber-grade recycled materials. Note that screen change frequency rises sharply at this precision. For high-impurity feeds, upgrade to candle filters or leaf filters for higher dirt-holding capacity.
Practical Reference: For poorly washed agricultural film, start with a 40/80 mesh combination. For clean industrial PP waste, use a single 120-mesh layer directly.
III. Structure Selection: Plain, Pleated & Composite Filters
Beyond flat round or square screens, pelletizing lines commonly use these specialized structures:
Multi-Layer Composite Screens
Consist of coarse support mesh + fine working mesh + protective mesh — e.g., 20 mesh + 120 mesh + 40 mesh. Coarse layers provide strength, fine layers perform filtration, and the working mesh is protected from damage. Suitable for most plastic recycling lines.
Pleated Filters
Greatly increase effective filtration area (3–5 times that of plain screens). For high-viscosity rubber melts or long production runs (e.g., 24-hour continuous operation), pleated filters significantly reduce screen change frequency.
Disc / Leaf Filters
Rigid, washable, and reusable filtration elements matched with leaf filter housings. High upfront investment but low long-term operating cost. Ideal for large continuous PET or PP recycling plants.
Matching Tips:
- For old lines with single-station manual screen changers, stick to standard multi-layer round screens — pleated types may cause edge leakage due to uneven compression.
- For lines with dual-column or non-stop screen changers, prioritize pleated filters to maximize service life.

IV. Material & Craft: Core Guarantee of Temperature & Pressure Resistance
Melt temperatures in recycling can reach 280°C (PET) and above, with instantaneous pressure spikes during screen changes exceeding 30 MPa.
- Wire Material: Must use 304 or 316L stainless steel wire. 316L offers superior corrosion resistance against residual acidic or alkaline substances in recycled feedstock.
- Weaving Method: Plain weave is most universal; twill weave has higher porosity but slightly lower stability. For rubber recycling, twill woven screens are recommended to resist collapse under high-viscosity melt.
- Edge Treatment: Finished filters must have argon-arc welded or crimped edges. Unfinished rough edges may burst under high pressure, allowing steel wire to contaminate pellets and cause severe quality defects.
V. Matching with Screen Changers & Sealing Systems
Your line configuration determines the exact format of screen filters.
- Manual / Hydraulic Plate Screen Changers Use standard round or square screens. Ensure edges fit perfectly with sealing surfaces. Add sealing rings or breaker plates to prevent leakage.
- Dual-Column Screen Changers Use cylindrical or cartridge-style pleated filters or candle filters. Inner diameter, length, and end-cap connections must be customized to the changer model.
VI. Economic Evaluation: Unit Cost vs. Total Operating Cost
Do not focus only on the unit price of screen filters. Professional buyers calculate filtration cost per ton of output.
Formula: Cost per ton = (Unit screen price ÷ Tons treated per screen) + Output loss from screen change downtime (USD/ton)
Suggestion: For mixed waste with fluctuating quality, prepare two solutions:
- Normal conditions: 120-mesh multi-layer composite screens to ensure quality.
- Heavily contaminated material: quickly switch to 60-mesh coarse screens + downstream fine filtration to avoid frequent shutdowns.

VII. Supplier Verification & Sample Testing
Before ordering, verify supplier capabilities using these steps (refer to professional manufacturers such as https://www.haigongplastic.com):
- Customization Proof: Check records for custom screen filters by material, size, and shape (e.g., high-temperature reinforced types for PET).
- Material Certification: Request third-party material test reports to confirm stainless steel grade and trace element content.
- Sample Trial: Order 50–100 sample screens (various mesh and structures) for on-line testing. Record:
- Initial pressure difference and time to alarm pressure
- Stability of die head pressure recovery after screen change
- Impurity distribution on used screens (to check for leakage)
Although small in size, screen filters play a decisive role in recycling and pelletizing lines. By starting with material analysis, relying on measured data, and verifying line compatibility, you can achieve the best balance among filtration precision, operating cost, and production efficiency. For demanding applications such as rubber recycling, consult suppliers for combined systems: candle filters for pre-filtration + pleated filters for fine filtration.