





0102030405
The Anatomy of an Extruder Screen Pack: Layers, Meshes, and Functions
2025-11-19
In polymer processing, the extruder screen pack operates as the final quality gate before molten material shapes into product. This seemingly simple disc determines surface finish, structural integrity, and production uptime. Understanding its layered architecture reveals why precision-engineered filtration directly correlates with throughput efficiency and defect reduction.
Multi-Layer Architecture: The Structural Foundation
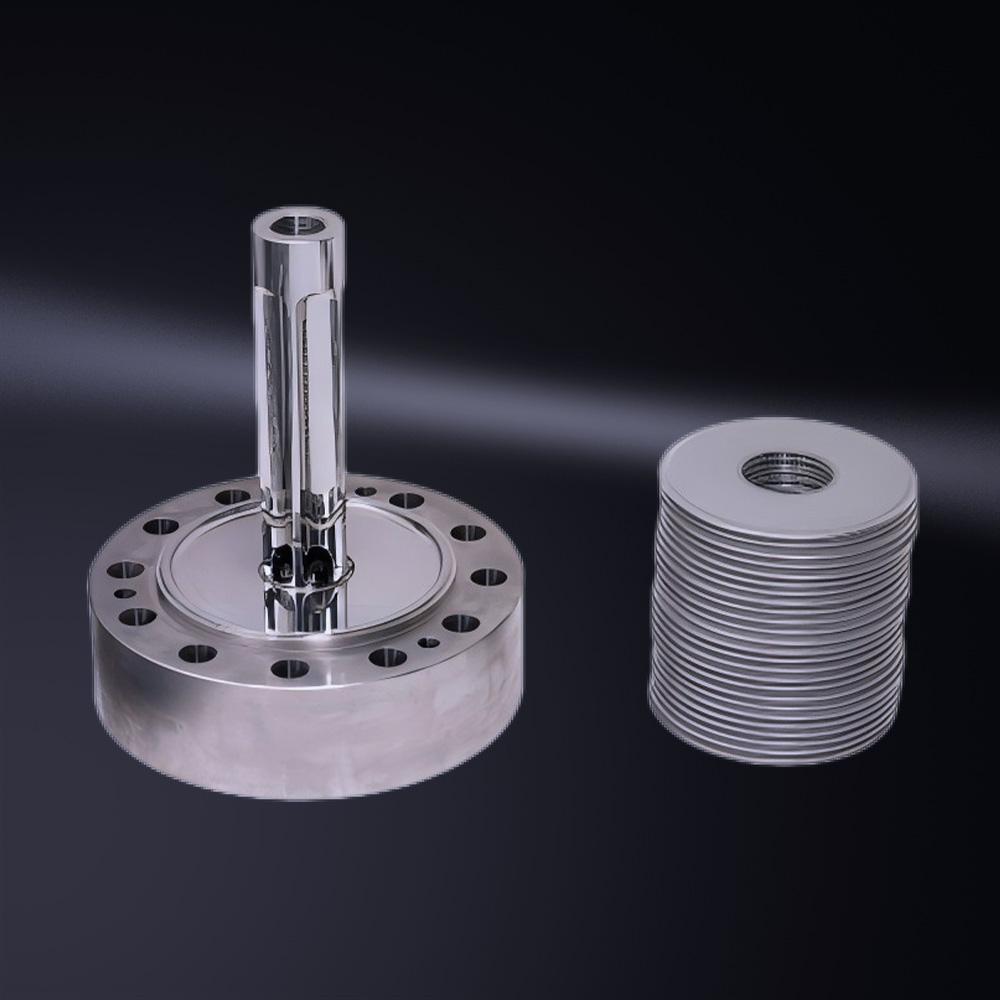
A standard screen pack functions as a composite filtration unit, typically comprising two to five discrete layers. Each layer serves a distinct mechanical purpose, creating a gradient that manages both pressure distribution and contaminant capture.
Support/Backing Mesh forms the upstream layer, characterized by coarse apertures (typically 10-40 mesh). This layer bears the primary brunt of melt pressure—often exceeding 5,000 psi in high-throughput applications—and prevents downstream collapse. Constructed from 0.25-0.50mm wire diameter, its role is structural rather than filtrative.
filtration mesh constitutes the core precision element. Square-mesh weaves from 60-500 mesh (with filaments as fine as 0.0635mm) trap gel particles, unmelted resin, and metallic contaminants. Multi-layer packs often sequence multiple filtration grades in descending order: for example, a 20/80/100/60 configuration positions the 100-mesh layer as the primary filter, flanked by 80-mesh upstream and 60-mesh downstream to capture dislodged particles and ensure even flow.
Distribution Layer sits at the melt entry point, using perforated plate or coarse dutch weave to prevent channeling. This layer ensures uniform velocity profile across the filter surface, eliminating dead zones that allow contaminants to bypass the fine mesh.
The layering sequence follows a critical logic: coarser meshes protect finer ones from pressure spikes, while the final downstream layer captures media fragments that might detach during operation. Reversing this sequence reduces filter life by up to 70% and increases pressure delta exponentially.
Mesh Topology: Weave Patterns and Performance Characteristics
Four primary weave architectures define extruder screen capability:
Plain Weave creates a simple over-under intersection, offering 1:1 thread count ratio. Economical for general-purpose filtration, it provides consistent open area (typically 35-40%) and suits applications where pressure drop must remain minimal. However, its geometric symmetry makes it vulnerable to wire migration under cyclic loading.
Dutch Weave inverts the diameter ratio—thick warp wires crossed by fine weft wires. Plain dutch weave (e.g., 12×64 mesh) achieves filtration ratings down to 20μm while maintaining structural rigidity. Twill dutch weave increases wire count to 14×100 or 16×120, enabling 5-10μm precision essential for optical-grade films and medical tubing. The asymmetrical structure locks wires in place, preventing aperture deformation at temperatures exceeding 300°C.
Sintered Mesh represents the premium tier. Multiple wire cloth layers undergo vacuum diffusion bonding at 1,200°C, creating a unified porous matrix. This eliminates individual wire movement entirely and delivers absolute filtration (β≥5000) for critical applications like battery separator films. Edge thickness ranges 1.5-3mm, providing inherent rigidity that often eliminates the need for external frames.
Perforated Plate serves as pre-filtration or structural backbone in recycling applications. With hole diameters from 0.5mm to 3mm, it stops large agglomerates before they load the fine mesh, extending filter life by 40-60% in post-consumer resin processing.

Material Selection: Chemistry Meets Thermal Dynamics
Austenitic stainless steels dominate extruder screen construction. AISI 304 handles general-purpose polymers up to 450°C, resisting oxidation and mild corrosives. AISI 316L becomes mandatory when processing fluoropolymers or materials containing halogenated flame retardants, as its 2-3% molybdenum content resists pitting corrosion.
In high-speed PET recycling, where acidic contaminants and moisture create aggressive conditions, some manufacturers specify Inconel 625 or Hastelloy C-276 for the finest mesh layer. These nickel-based alloys maintain tensile strength above 800MPa at 500°C, though they increase material cost by 8-10x.
Frame materials present another critical choice. Aluminum 1100-O (soft temper) rims allow spot welding without embrittling the mesh, while stainless steel 304 frames suit automatic screen changers where magnetic handling requires ferrous compatibility. Rubber-framed variants provide compression sealing in low-pressure (<1,000 psi) blown film extrusion.
Edge Engineering: From Spot Welds to Encapsulation
Edge treatment determines pack integrity under pressure cycling. Spot Welding creates discrete fusion points at 6-12 locations around the perimeter. For three-layer packs, welding sequence affects durability—welding the outer layers first, then the middle, prevents inter-layer shear. Automated resistance welding controls current density to avoid wire burn-through, maintaining 90% of base metal strength.
Encapsulated Frames involve pressing the mesh stack into an aluminum or stainless channel, then crimping or welding the rim. This distributes clamping force evenly, preventing the "potato chip" deformation common in unsupported packs at pressures above 3,000 psi. Frame thickness typically matches breaker plate groove width within +0.05mm tolerance to ensure positive seal.
For continuous screen changers (CSC), trapezoid or kidney shapes slide through sealing lands. Here, edge finishing requires surface grinding to Ra 1.6μm to prevent polymer leakage and minimize frictional wear on sealing surfaces.
Functional Performance: Pressure, Flow, and Contaminant Management
The pack's pressure differential (ΔP) follows Darcy’s law modified for compressible media. A 3-layer 40/100/40 configuration exhibits ΔP of 150-200 psi at 500 lb/hr throughput with virgin resin. Contaminant loading increases ΔP linearly until the "blinding point" where capture efficiency drops precipitously.
Flow distribution is quantified by uniformity index (UI). Well-designed packs achieve UI > 0.92, measured by thermographic mapping of melt temperature across the die width. Poor UI manifests as gauge bands, melt fracture, or additive streaking.
Contaminant capacity—the mass of debris retained before failure—depends on layer porosity gradient. A 20/80/100/60 pack captures 2.8-3.5 g/in² of metallic particles (150-500μm) before breakthrough, whereas a single-layer 100-mesh screen saturates at 0.4 g/in².

Application-Specific Configurations
Film Extrusion (15-50μm gauge) demands absolute gel elimination. Four-layer packs using 60/120/200/80 dutch weave maintain clarity while processing LLDPE. The 200-mesh layer operates at its mechanical limit, requiring sintered construction to prevent mesh extrusion.
Pipe/Profile Extrusion prioritizes pressure stability. Two-layer 20/40 plain weave packs handle regrind content up to 30% while keeping ΔP below 100 psi, preventing melt temperature rise that degrades PVC stabilizers.
Recycling Operations battle heterogeneous contamination. Five-layer stacks (10/20/40/100/40) with perforated plate backing process washed flakes containing paper labels and aluminum fragments. The graduated structure prevents sudden blinding, extending filter life to 8-12 hours versus 2-3 hours for single-layer designs.
Medical Tubing requires validated extractables performance. Sintered 316L packs with electropolished surfaces reduce particle shedding to <50 particles/cm³ >10μm, meeting USP Class VI requirements.
Selection Criteria: Matching Pack to Process
Choosing the optimal configuration requires analyzing five parameters:
- Contaminant Load: High regrind content demands coarser upstream protection
- Pressure Budget: Fine meshes increase ΔP; oversized packs waste material
- Temperature Profile: Sintered meshes handle >400°C continuous duty
- Change Frequency: Automatic changers justify premium packs; manual changes favor economical spot-welded designs
- Product Criticality: Optical clarity necessitates dutch weave; structural profiles permit plain weave
Computational fluid dynamics (CFD) modeling now predicts pack performance before installation. By simulating particle trajectories and pressure fields, engineers optimize layer sequence without costly trial-and-error. Leading manufacturers provide digital twins of their screen packs, integrating directly into extrusion simulation software.
Maintenance and Failure Analysis
Even the finest pack fails if misused. Pressure spikes during startup cause "wire draw"—fine mesh extruding through coarser layers. Preheating the pack to melt temperature before applying full pressure prevents this. Cleaning protocols depend on material: pyrolysis ovens at 450°C remove polyethylene; chemical baths dissolve PET without attacking stainless steel.
Failure modes provide diagnostic data. Uniform blinding across the radius indicates excessive contaminant load. Edge-heavy contamination suggests poor sealing or channeling. If the downstream layer shows more loading than upstream, the pack is installed backwards—a surprisingly common error costing 20-30% efficiency loss.
Conclusion
The extruder screen pack embodies engineered precision where micrometer-scale differences define success. Its layered anatomy—support, filtration, distribution—mirrors the complexity of polymer science itself. As extrusion pushes toward Industry 4.0 integration, with pressure sensors embedded in breaker plates and AI predicting optimal change intervals, the fundamental physics remain unchanged: graduated filtration, material compatibility, and structural integrity.
Understanding these principles enables processors to match screen pack architecture to product requirements, reducing waste, increasing uptime, and achieving the dimensional consistency modern markets demand. The investment in correctly specified filtration pays measurable dividends in quality metrics and operational stability.