





0102030405
Raw Material Cost: High-Temp vs. Standard Filter Media
2026-07-29
In the procurement cycle for Polymer Melt Filtration Systems, Leaf Filters, Candle Filters, and Pleated Filter Elements, understanding the Raw Material Cost Gap Between High Temperature and Standard Filter Media is the primary variable dictating the final quotation. For global engineering procurement officers, polymer distribution agents, and extrusion line maintenance teams comparing 304 Woven Wire Mesh, 316L Sintered Felt, 310S Heat-Resistant Felt, FeCrAl Fiber Felt, and Hastelloy C276 Filter Elements, the focus must shift from the unit price of the finished good to a holistic view of alloy base prices, fiber preparation, sintering technology, cleanability, and Total Cost of Ownership (TCO). This analysis breaks down the RFQ review process from a buyer's perspective.
1. Establishing the Cost Baseline: Standard Filter Media
For conventional operating conditions (Room Temperature to 400°C, low corrosion), 304 Stainless Steel woven wire mesh or multi-layer sintered mesh serves as the industry benchmark. Based on current market trends, 304 stainless steel round bars average approximately $2,200–$2,300 USD per metric ton, while cold-rolled plates range between $1,800–$2,150 USD/MT. With a nickel content of around 8%, 304 offers the lowest alloy surcharge.
Building on this baseline:
- 304 Woven Mesh Pleated Elements: These utilize thicker wires and faster weaving speeds. Raw material costs are minimal, making them the most economical choice for polymer pre-filtration and extrusion screen packs.
- 304 5-Layer Sintered Mesh: Adding vacuum sintering and calendaring increases process costs significantly. Standard sheets typically range from $25–$55 USD per square meter.
- Upgrading to 316L: To enhance corrosion resistance (specifically against chlorides), 316L incorporates 2–3% Molybdenum and increases Nickel to 10–14%. This elevates raw material costs to roughly $3,400–$3,600 USD/MT (a 35–55% premium over 304). Consequently, a finished 316L 5-layer sintered mesh filter generally costs 18–25% more than its 304 counterpart.
2. The Cost Escalation Curve: High-Temperature Filter Media
When applications move into extreme temperatures (400–1200°C)—such as polymer melt processing (280–320°C), film stretching ovens, petrochemical cracking, or high-temperature exhaust gas—material selection jumps exponentially in cost:
- 310S Heat-Resistant Stainless Steel: With 24–26% Chromium and 19–22% Nickel, 310S round bars cost approximately $3,900–$4,100 USD/MT. This represents a 75–95% increase over 304 and 15–25% over 316L. Expect 310S sintered mesh prices to be over 40% higher than 304 equivalents.
- 316L Stainless Steel Fiber Felt: Unlike woven mesh, this media consists of randomly laid metal micro-fibers sintered together, offering high porosity and dirt-holding capacity—ideal for high-viscosity polymer melts. Market prices range from $12–$380 USD per square meter, driven by grammage and layering. The cost of drawing wire rod into micro-fibers and the associated yield loss contribute heavily to this price.
- 310S Fiber Felt & FeCrAl Fiber Felt: Designed for 1000–1200°C, FeCrAl (Iron-Chromium-Aluminum) alloys offer lower raw material costs than nickel-based alloys, but the complexity of fiberization offsets some savings. 310S fiber felt typically adds another 20–35% to raw material costs compared to 316L fiber felt.
- Hastelloy C276 & Inconel Alloys: The ultimate nickel-based solution. Hastelloy C276 plate currently trades at $53,000–$63,000 USD/MT—15–18 times the cost of 316L. Reserved exclusively for severe corrosive and high-temperature environments (gasification, desulfurization, fluorochemicals), finished C276 filter elements often exceed $1,000 USD per unit, excluding specialized machining and welding gas costs.
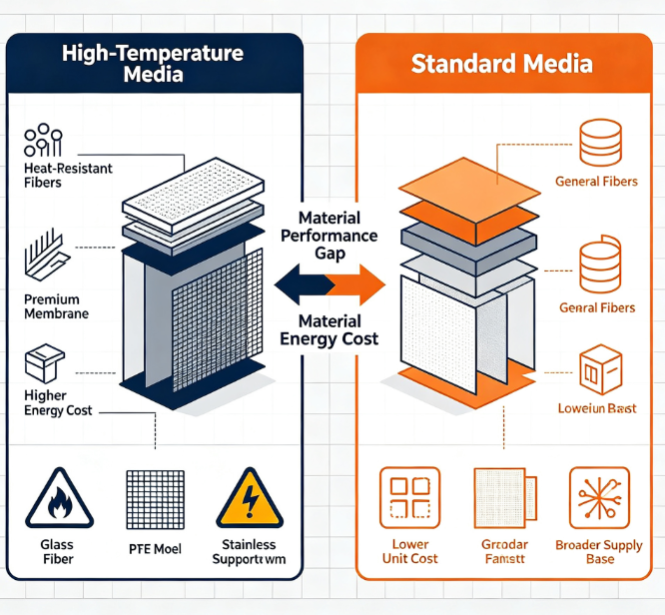
3. Understanding the Step-Function of Pricing
A common misconception among buyers is the assumption of linear cost progression (e.g., "every 100°C increase adds 10% to the price"). The reality is a series of step-function increases:
- 304 → 316L: Corrosion allowance adds 35–55% to raw material costs.
- 316L Mesh → 316L Sintered Felt: Switching from weaving to fiberization/sintering can multiply media costs by 1.5x to 3x.
- 316L Series → 310S Series: Changing Cr/Ni ratios adds 75–95% to raw material costs.
- 310S Mesh → 310S Fiber Felt: Adds another 20–35%.
- Entering Nickel-Based (C276): Represents an order-of-magnitude increase, not a percentage scaling.
Furthermore, increasing filtration precision (e.g., from 100µm to 10µm) drastically reduces production yields during fine-wire weaving and uniform sintering, potentially adding 2x to 5x in process costs.
4. Translating Raw Material Costs into Lifecycle Value
Focusing solely on the purchase price is a tactical error. While a 310S filter element might cost nearly double a 304 element, using 304 in a 300°C polymer melt environment leads to carbonized gel formation that cannot be backflushed. The resulting downtime and change-out costs often exceed the filter price difference by tenfold. Conversely, although 316L sintered felt carries a higher initial capital expense, its ability to withstand offline calcination and online backwashing extends service life to 3+ years. When amortized, the annual cost is frequently lower than replacing cheaper 304 elements annually.
Strategic RFQ Tip: Insist that suppliers break down quotations into three distinct lines:
- Raw Media Cost (per m², including alloy grade and grammage).
- Sintering & Forming Fees.
- Hardware Costs (End caps, seals, support cages, laser welding).
This transparency reveals exactly where the budget is allocated, preventing opaque "high-temp premiums."
5. Strategic RFQ Writing for Price Lock-In
To avoid vague "High-Temp Filter" line items, structure your inquiry with precise technical parameters:
- Max/Average Operating Temperature.
- Chemical Exposure (Chlorides, Acids, Solvents).
- Filtration Rating (Microns).
- Requirement for Backwash/Cleanability.
- Medium Type (Polymer Melt, Gas, Liquid).
- Desired Continuous Run Cycle.
Request parallel quotes for:
- 304 5-Layer Sintered Mesh
- 316L Sintered Felt
- 310S Fiber Felt
- FeCrAl Fiber Felt (if >800°C)
This comparative grid forces transparency and prevents suppliers from applying arbitrary "high-temperature" markups.
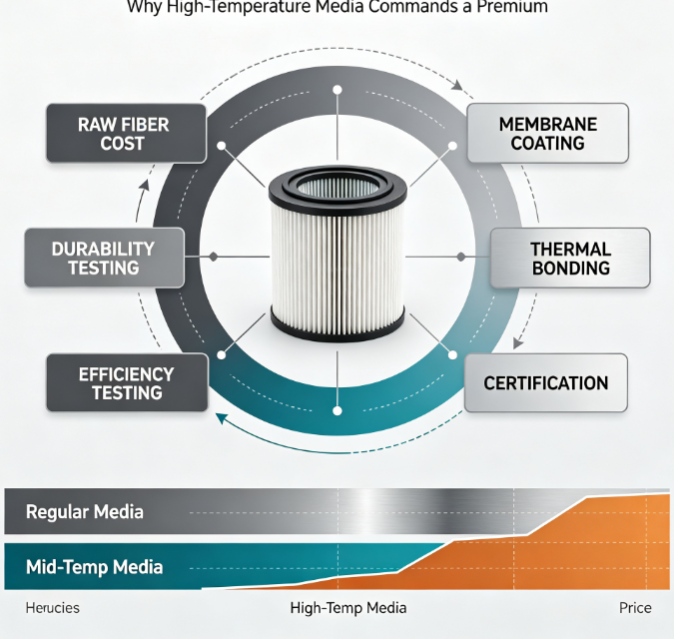
6. Contractual Safeguards Against Alloy Volatility
Nickel prices are notoriously volatile. Historically, a 10% increase in Nickel results in approximately a 3% rise in 316L costs and up to an 8% rise in Hastelloy C276 costs. When negotiating bulk imports of Candle Filter Cartridges or Leaf Discs, include a price adjustment clause tied to the LME (London Metal Exchange) Nickel Price or the mill's official price list (trigger point: ±5% fluctuation). Additionally, specify the Mill Origin (e.g., TISCO 310S, Imported 316L Micro-Wire) to prevent material substitution.
7. Conclusion: Cross-Tabulating for Optimal Selection
The Cost Gap Between High-Temperature and Standard Filter Media is fundamentally driven by four factors: Chromium/Nickel/Molybdenum ratios, fiberization complexity, sintering yield rates, and regeneration lifespan. 304-grade media remains the optimal choice for low-temperature, mild-corrosion environments. 316L Sintered Felt represents the industry's workhorse for polymer melt filtration. 310S and FeCrAl are engineered for oven and cracking furnace extremes, while Hastelloy is reserved for the most aggressive chemical processing conditions. By cross-referencing temperature requirements with chemical exposure tables, procurement managers can select the most economically viable technical solution rather than simply chasing the lowest bid or the highest temperature rating.