





0102030405
Top Candle Filter Cartridge Suppliers for PP/PE Recycling
2026-07-23
In the pelletizing production lines for recycled polypropylene (PP) and polyethylene (PE) waste plastics, candle Filter Cartridges sit at the core of the melt filtration system. Their role is not to trap sediment in clean water or slurry, but to continuously capture residual paper ash, carbonized spots, aluminum foil fragments, unmelted gels, and hard particles from broken screens—all within polymer melts at 200–300°C and viscosities ranging from hundreds to tens of thousands of centipoise. Once filter precision drifts or welds crack, downstream die heads, spinning components, and BOPP film lips will clog within hours; the cost of unplanned line downtime far exceeds the price of the cartridges themselves. Therefore, when evaluating candle filter cartridge suppliers for PP/PE recycling lines, buyers must codify four non-negotiable criteria into contract annexes: traceable materials, verifiable precision, predictable differential pressure, and reusable cleanability—rather than relying solely on catalog claims like “304 stainless steel, 20 microns.”
Special Operating Boundaries for PP/PE Recycled Melt Filtration
Feedstock for recycled PP/PE comes from diverse sources: supermarket films, agricultural films, milk bottles, chemical drums, and cable sheathing are mixed together. Even after washing, ash, SiO₂ fillers, and TiO₂ masterbatch residues remain. Typical line operating conditions are as follows:
- Melt temperature: PP ~200–260°C, PE ~180–240°C (lower for LDPE, higher for HDPE).
- System differential pressure: Front-end working pressure of continuous screen changers typically 0.3–2.0 MPa. Maximum allowable pressure for metal-sintered cartridges can reach 10–21 MPa (210 bar), but PP/PE recycling lines usually set alarm thresholds at 1.5–3.0 MPa for screen cleaning.
- Contaminant morphology: Dominated by hard inorganic particles and coexisting gels—unlike esterified sticky gels in PET recycling. Thus, cartridge structures favor surface capture + shallow dirt holding, rather than ultra-deep dirt retention of metal fiber felts.
- Line rhythm: Recycling lines are mostly single-pass; less sensitive to differential pressure curves than continuous filament spinning. However, screen change frequency directly impacts labor costs. Every 0.02 MPa reduction in initial cartridge pressure drop extends cleaning cycles by over 10%.
Understanding these boundaries is critical to judging whether a supplier’s push for “5-micron metal fiber sintered felt pleated candle cartridges” constitutes over-specification.

Cartridge Structure Types: Roles of Smooth Cylindrical, Pleated, and Plum-Blossom Skeleton Designs
Three common candle structures are used in PP/PE recycling lines; procurement lists must specify them by workstation:
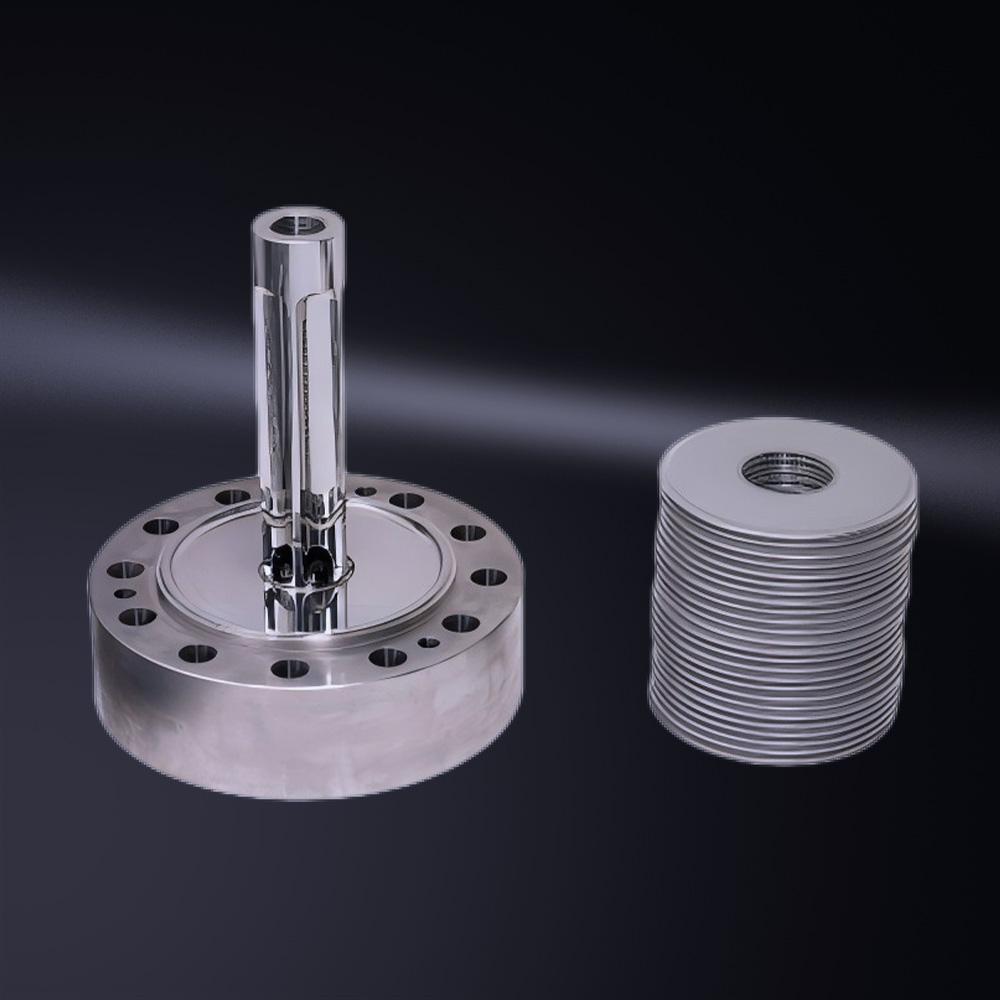
- Cylindrical multi-layer wire mesh candle cartridges: Outer layer 180–325 mesh twill dutch weave, middle support layer 20–50 mesh coarse mesh, inner perforated tube—fully welded, no adhesives. Precision: 20–100 microns (primary range). Best cost-performance; ideal for coarse filtration in bottle flake recycling and pre-screen changer stages.
- Pleated candle cartridges: Filter area 3–5x larger than smooth tubes at the same outer diameter, with lower initial pressure drop. Suited for high-cleanliness applications like film recycling (PP/PE blown film edge trims); precision down to 5–25 microns.
- Plum-blossom/petal skeleton cloth-covered cartridges: Mostly used for solution or low-temperature solid-liquid separation; rarely used in PP/PE melt lines—unless the line includes post-stage slurry washing processes.
A common procurement pitfall is overusing pleated cartridges, leading to deep gels clogging pleat corners that cannot be removed by backflushing, resulting in more frequent replacements than smooth tubes. The correct approach is a two-stage setup: coarse filtration with 40–75 micron smooth tubes + fine filtration with 20–25 micron pleated cartridges.
Material & Filter Media: Tradeoffs Between 304L/316L and Sintered Felts
International standard specifications for melt candle cartridge materials:
- End caps, center tubes, support meshes: 304, 304L, 316, 316L stainless steel per ASTM A240. PP/PE has no strong chloride corrosion; 304L is sufficient. 316L may be used for coastal high-humidity packaging shops with full machine washing.
- Primary filter layers: Stainless steel twill dutch weave covers 10–100 microns; stainless steel fiber sintered felts cover 1–15 microns (for non-woven PP lines). Suppliers quoting “200 mesh” as “20 microns” are immediate disqualifiers. Each batch must include bubble point tests (per ISO 2942) and airflow reports to verify actual absolute precision ratings.

Dimensions & Connections: Reverse-Engineer to Existing Filter Chamber Specifications
Filter chamber dimensions in recycling line screen changers are fixed. Buyers must provide suppliers with precise specs—not just “a candle cartridge”:
- Outer diameter: Common sizes Φ42 mm, Φ46.5 mm, Φ50 mm, Φ60 mm, Φ100 mm.
- Length: 460 mm, 512 mm, 750 mm, 1150 mm (copy original chamber dimensions; tolerance ±0.5 mm).
- Connections: Thread M27×1.5, 226 bayonet, flange, rod connection, custom welded end caps.
- Flow direction: Outside-in is standard; reverse flow will collapse filter layers.
- Laser marking: Batch number, material, precision, and length engraved on end caps for traceability.
Many downtime incidents stem from “2 mm excess length jamming chamber lids” or “incorrect thread pitch causing half-turn thread failure.” These can be caught via full CMM inspection during the PPAP sample stage.
Cleaning Regeneration & Lifespan: Quantify “Cleanable” as Cycles
A key selling point of metal candle cartridges is regenerability via backflushing, ultrasonics, and calcination. Procurement specifications must clearly state:
- Allowed cleaning methods: High-pressure melt backflush, ultrasonic alkaline washing, furnace burning at 450°C for carbon removal (metal parts only).
- Post-regeneration precision recovery rate: ≥ 90% of new cartridge absolute precision.
- Lifespan benchmarks: Smooth tube cartridges in PP bottle flake lines typically run 7–20 days at 0.8 MPa average pressure (depending on feedstock cleanliness); pleated felt cartridges last 30–60 days but degrade faster after cleaning.
- Scrap criteria: Bubble point fails nominal precision rating, melt leakage through welds, center tube deformation.
Supplier claims of “long service life” are meaningless without a reference customer replacement cycle distribution table for identical operating conditions.

Five Original Documents for Supplier Due Diligence
Before signing a bulk framework agreement, obtain the following originals from candidate factories:
- ISO 9001 certificatewith scope including “sintered Filter Element / wire mesh candle.”
- Material MTC: 304L/316L furnace batch spectral analysis, with verified Ni ≥ 8% (304 series).
- Batch bubble point + airflow test reports (per ISO 2942, ISO 3968).
- Operational case studies for similar PP/PE recycling lines (confidential data redacted; operating parameters provided).
- Welding process cards: Full welding (no adhesives), no silver solder residue, end cap laser or argon arc welding parameters.
Suppliers providing only catalog images—no MTC or bubble point reports—are unqualified for melt-grade supply.
Assortment Strategy Backward-Engineered by End Production Lines
Distributors/engineering firms are recommended to match candle cartridge platforms to three line types:
- PP woven bag/ton bag recycling pelletizing lines: Φ42×460 smooth tube, 75 μm absolute, 304L, threaded connection—volume-driving SKU.
- PE film/LDPE agricultural film recycling blow-molding lines: Φ46.5×512 pleated, 25 μm, 316L end caps, outer protective mesh.
- PP spunbond non-woven edge trim recycling lines: Φ60×750 sintered felt, 10 μm absolute, full 316L, laser traceability.
If a single supplier can cover all three tiers with shared end-cap processes, pilot orders should test “200 pcs 75 μm smooth tubes + 50 pcs 25 μm pleated cartridges” instead of over-specifying 20 μm across the line, which causes frequent screen changes.

Final Selection Bottom Line
Provide the supplier with three critical data points: line melt temperature, screen changer alarm differential pressure, and original chamber length/thread specs. Require them to return a filter layer structure table and bubble point report. Suppliers who cannot deliver are not the right candle filter cartridge providers for PP/PE recycling lines.